
- NAS 965 Type DFull standard compliance (1/4-28 UNF-2A)
- 5,000+ ItemsComplete wire, fraction, letter & metric stock
- CAGE 0PFP1Approved U.S. Defense & Global Aerospace Vendor
- TIR < 0.0005"Ultra-precision concentricity for zero chatter
Precision Hole-Making in Confined Aircraft Envelope Geometries
In aerostructure manufacturing, line-fit assembly, and military/commercial depot maintenance (MRO), tooling engineers and structural technicians encounter restrictive access envelopes where conventional straight-shank jobber drills held in keyless chucks cannot operate. National Aerospace Standard NAS 965 Type D threaded shank adapter drills solve this fundamental physical bottleneck.
Kinematic Efficiency of 1/4-28 Threaded Mating
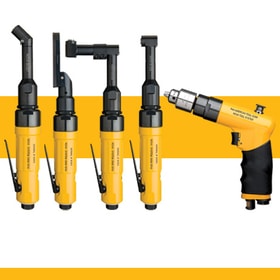
By incorporating a precision ground 1/4-28 UNF-2A male thread directly onto the tool shank, NAS 965 drills thread seamlessly into female spindle drives of low-profile 45°, 90°, and 360° angle air motors—such as our proprietary Nova® Pneumatic Aircraft Tools. This direct mechanical coupling eliminates bulky drill chucks, reduces overall tool protrusion by up to 70%, and provides rigid axial alignment under heavy thrust loads.
Furthermore, NAS 965 drills feature an integrated driving flat across the threaded shank. This flat enables positive mechanical locking with open-end wrenches, ensuring non-slip torque transfer when machining high-strength aerospace alloys. The result is total elimination of shank slippage—a primary cause of hole scoring, work hardening, and catastrophic tool failure in tough titanium (Ti-6Al-4V) and nickel-based superalloy (Inconel® 718) airframe structures.
- Elimination of Spindle Runout: Concentricity ground to Total Indicator Reading (TIR) under 0.0005 in.
- Integrated Microstop Compatibility: Seamlessly mounts inside microstop countersink cages for depth-controlled countersinking and drilling.
- Web Reduction Geometry: 135° split point minimizes axial thrust force, preventing sheet deflection and burr formation on exit.
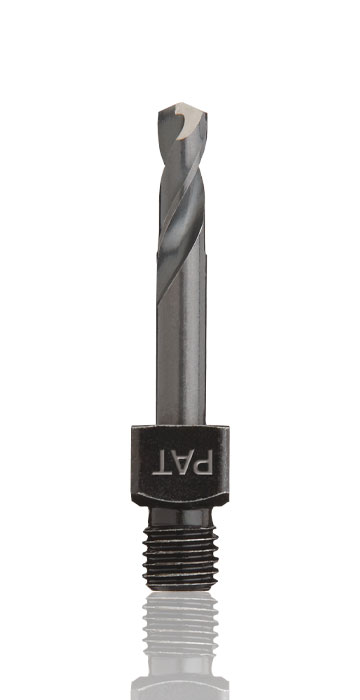
NAS 965 Type D Dimension Envelope
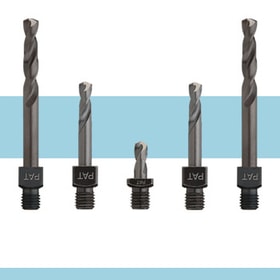
Manufactured strictly according to U.S. National Aerospace Standards, covering five standardized length configurations:
- Very Stubby: 1-1/8" Overall Length (OAL) — Maximum rigidity in tightest ribs
- Stubby: 1-1/4" Overall Length (OAL) — Standard skin repair choice
- Short: 1-1/2" Overall Length (OAL) — Balanced reach and torsional strength
- Long: 2-1/8" Overall Length (OAL) — Deep pocket clearance
- Extra Long: 2-3/4" to 3-1/2" OAL — Extended reach through multiple ribs
NAS 965 Product Portfolio: Material Options & Dimensional Range
Pan American Tool Corporation manufactures and inventories the industry's most comprehensive line of NAS 965 Type D drills. Every tool is produced under rigorous ISO 9001 quality frameworks, backed by full lot traceability and material test certifications.
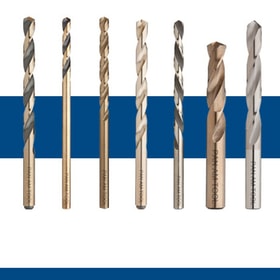
M42 8% Cobalt NAS 965 Drills
Request Quote ›
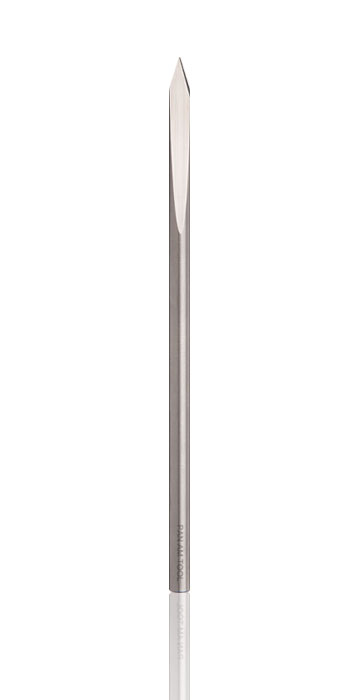
Solid Carbide NAS 965 Drills
Request Technical Datasheet ›
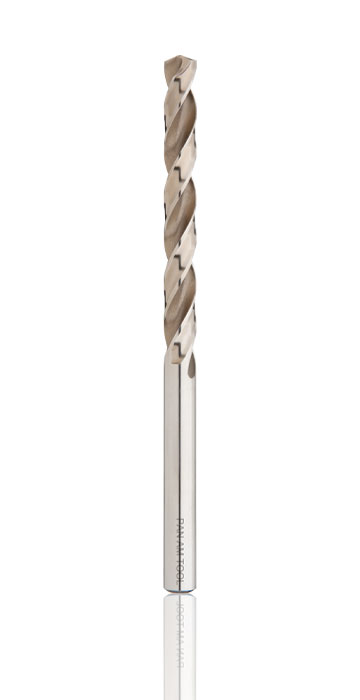
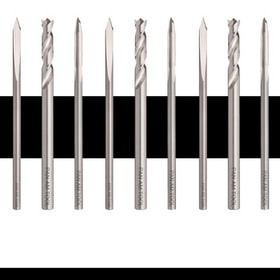
Double Margin NAS 965 Drills
Inquire Now ›
| Workpiece Alloy Grade | Substrate Class | Surface Speed (SFM) | Feed Rate (IPR) by Diameter Range | Coolant / Lubrication Strategy |
|---|---|---|---|---|
| 2024-T3 / 7075-T6 Aluminium | M42 Cobalt / HSS | 250 – 350 SFM | .002" (#40) – .008" (1/4") – .012" (7/16") | Mist Lubricant / Soluble Oil Spray |
| Titanium Ti-6Al-4V (Grade 5) | M42 8% Cobalt | 40 – 60 SFM | .001" (#40) – .003" (1/4") – .005" (3/8") | Flood Coolant or High-Pressure Air/Oil Mist |
| Inconel 718 / Rene 41 | M42 8% Cobalt | 20 – 35 SFM | .0008" (#30) – .002" (1/4") – .004" (3/8") | Continuous Active Sulfur Oil / Flood |
| CFRP Composite Panels | Solid Carbide | 300 – 500 SFM | .0015" (#40) – .004" (1/4") – .006" (3/8") | Vacuum Vacuuming / Dry Air Blast Only |
| CFRP / Titanium Stack-ups | Solid Carbide (Dagger Geometry) | 50 SFM (Ti) / 200 SFM (CFRP) | Controlled Constant Mechanical Feed .002" | Minimum Quantity Lubrication (MQL) |
Future B2B Procurement Trends in Aerospace Cutting Tooling (2025–2035)
As global aerospace original equipment manufacturers (OEMs) like Boeing, Airbus, Lockheed Martin, and Embraer ramp up narrowbody and widebody build rates while airlines accelerate fleet maintenance, cutting tool procurement strategies are undergoing a fundamental transformation.
1. Shift Toward Multi-Material Stack Optimization
Modern airframes utilize multi-material structural joints combining carbon fiber composites, titanium sub-structures, and aluminum-lithium skins. Procurement teams are moving away from single-purpose drills toward hybrid-geometry NAS 965 drills. Cutting tools must now drill clean, delamination-free entry holes through CFRP without burning or fraying fibers, then instantly transitions to cutting solid titanium without heat-induced work hardening—all in a single automated or manual stroke.
2. Automated Drilling Units (ADUs) & Robotic Integration
Tier-1 aerostructure assemblers are rapidly adopting portable Automated Drilling Units (ADUs) and multi-axis articulated robots on the factory floor. These systems demand NAS 965 threaded shank tools manufactured to micro-inch dimensional repeatability. Dynamic tool wear monitoring, standardized length presets, and zero-runout shanks are mandatory requirements to prevent unplanned line stoppages in high-rate assembly lines.
3. Supply Chain Resilience & Digital Vendor Integration
Global supply disruptions have elevated vendor reliability to a primary procurement KPI. Procurement directors are consolidating vendor lists, favoring established U.S. manufacturers with extensive shelf inventory, active CAGE Codes (0PFP1), and real-time EDI/API inventory integration. Stock availability of specialized wire and letter sizes in NAS 965 configurations ensures MRO aircraft-on-ground (AOG) events are resolved within hours rather than weeks.
Technological Evolution & Next-Generation Tooling Advances
The humble threaded shank drill has evolved dramatically from early High-Speed Steel (HSS) designs. Ongoing advancements in metallurgy, PVD nanostructured coatings, and automated CNC grinding geometries continue to extend tool life boundaries.
Sub-Micron Substrates & Advanced PVD Nano-Coatings
Traditional M2 steel tooling is rapidly being superseded by ultra-fine grain M42 8% Cobalt and nano-structured Solid Carbide. Furthermore, chemical surface treatment has given way to Physical Vapor Deposition (PVD) nano-coatings tailored for specific aerospace material groups:
- Titanium Aluminum Nitride (TiAlN / AlTiN): Extreme thermal barrier coating allowing dry or MQL high-speed drilling in heat-resistant superalloys.
- Diamond-Like Carbon (DLC) & Nanocrystalline Diamond: Hardness ratings up to 10,000 HV, reducing friction to near zero when drilling highly abrasive composite laminates, dramatically delaying edge rounding.
- Titanium Diboride (TiB2): Specialized anti-friction coating designed to eliminate chip adhesion and built-up edge (BUE) when machining soft, gummy aluminum alloys.
Precision Grind Geometry & 3D Flute Profiling
Modern 5-axis CNC grinding technology allows Pan American Tool engineers to sculpt complex flute profiles with variable helix angles and parabolic flute geometry. These features accelerate chip evacuation out of deep structural pockets, preventing chip packing—the primary driver of tool breakage in small-diameter (#40 to #10) threaded shank drills.
Information Gain: Concentricity & Torque Limits
Did you know? NAS 965 specifications require a pitch diameter tolerance on the 1/4-28 UNF-2A thread of 0.2248 to 0.2268 inches. Excess thread clearance leads to angular wobble, amplifying total indicated runout (TIR) at the drill point. Pan American Tool ground-from-solid thread manufacturing guarantees thread concentricity to shank axis within 0.0003 inches, delivering uncompromised hole roundness and tool life extension.
Frequently Asked Questions by Global Aerospace Buyers & Engineers
Direct technical answers to the most common questions raised by procurement managers, MRO engineers, and automated assembly planners when specifying NAS 965 tooling.
What are the precise thread standards and pitch tolerances for NAS 965 Type D drills?
Why are NAS 965 threaded shank drills preferred over straight shank drills in close-quarter aerospace assembly?
How does M42 8% Cobalt compare to Solid Carbide for NAS 965 drills in mixed-material airframe stacks?
What overall length classifications are defined under National Aerospace Standard NAS 965?
What is the primary root cause of shank shear at the 1/4-28 thread neck during hand-held angle motor drilling?
How does a 135° split point geometry reduce thrust force in titanium skin drilling?
Can NAS 965 threaded shank drills be used inside microstop countersink cages?
What documentation and quality certifications accompany Pan American Tool NAS 965 shipments?
Why Global Aerospace Leaders Partner with Pan American Tool
Since 1986, Pan American Tool Corporation has stood as an authoritative manufacturer and master distributor of specialized aviation cutting tools and pneumatic machinery. Operating out of our modern facility in Fort Lauderdale, Florida, we support commercial airlines, defense depots, Tier-1 aerostructure integrators, and MRO stations in over 80 countries.
- Decades of Manufacturing Heritage: Over 39 years dedicated exclusively to solving aviation drilling, reaming, countersinking, and fastening challenges.
- Official Defense Vendor Status: Designated CAGE Code 0PFP1, supplying U.S. Armed Forces, NATO defense contractors, and foreign military sales (FMS) programs.
- Unrivaled Inventory Depth: Over 5,000 distinct line items maintained in stock, eliminating long lead times for specialized aerospace drill sizes.
- Integrated Tool Systems: We manufacture both the pneumatic drives (Nova® Pneumatic Tools) and the cutting tools (NAS 965 Drills), offering single-source system accountability.
Global Commercial & Defense Logistics
Our experienced export logistics desk manages hazardous material declarations, customs clearance, ITAR compliance, and international freight consolidation to ensure fast delivery to hangars worldwide.
Corporate Headquarters & Distribution Center
Pan American Tool Corporation
5990 NW 31st Avenue
Fort Lauderdale, FL 33309-2208, USA
Toll-Free: 800-423-2764 | Int'l: +1-954-735-8665
Explore Complementary Aerospace Hole-Making & Finishing Categories
Maximize your assembly efficiency by pairing NAS 965 threaded shank drills with our complete range of precision aerospace cutting tools and pneumatic angle drives.

Need Custom NAS 965 Tooling Geometries or Large Bulk Quotes?
Connect directly with our Fort Lauderdale application engineering team. We provide rapid technical support, custom NAS 965 drill grinds, and volume pricing for international airlines and aerospace OEMs.