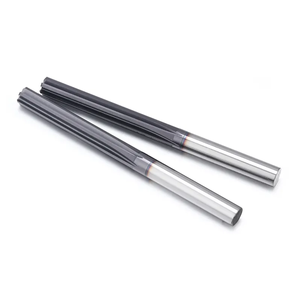
Supplying Puget Sound’s aerospace, marine engineering, and advanced medical hardware manufacturers with high-gain tooling options engineered to micro-inch surface finishes ($Ra < 0.4 \mu m$).
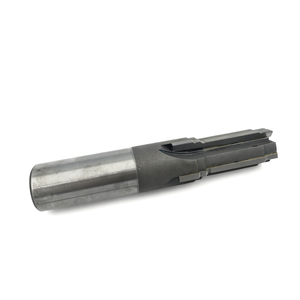
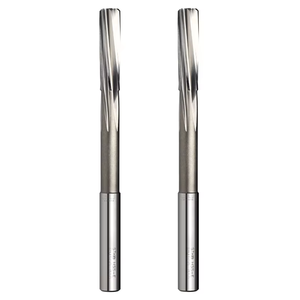
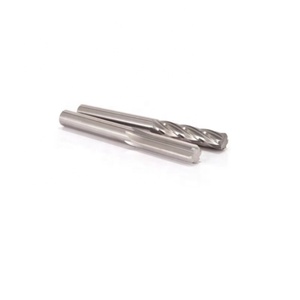
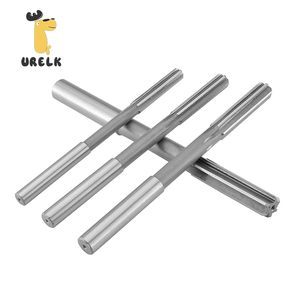
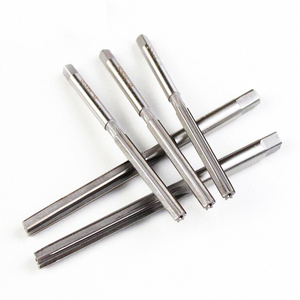
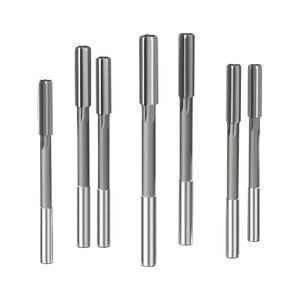
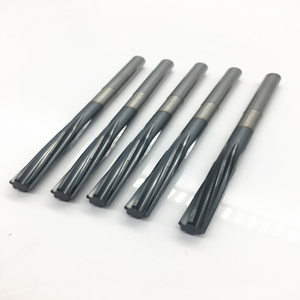
The Greater Seattle region—spanning Everett, Renton, Bellevue, Kent Valley, and Tacoma—stands as one of the world's primary nodes for commercial aviation manufacturing, space exploration hardware, marine propulsion engineering, and clean-tech innovation. With Tier-1 and Tier-2 aerospace machine shops supplying critical structural components for the Boeing 737 MAX, 787 Dreamliner, and naval defense programs, the requirements for hole-finishing tools have shifted from standard commercial grades to high-gain micro-grain carbide and STK/M42 HSS-E chucking reamers.
Achieving structural integrity in aerospace wing spars, hydraulic actuator blocks, landing gear pivot pins, and carbon-fiber composite (CFRP) titanium stacks demands reamers capable of holding strict diameter tolerances (H6, H7, and IT7 standards) while maintaining zero surface micro-cracking. As a leading Chinese manufacturer and direct exporter to Washington State, our factory bridges the gap between OEM-level precision and competitive direct-to-shop pricing.
To eliminate tool chatter, work hardening, and early edge breakdown in hard-to-machine alloys like Ti-6Al-4V, Inconel 718, 7075-T6 aluminum, and 316L stainless steel, our engineering team utilizes Swiss ANCA and Walter 5-axis CNC grinders with customized geometry setups:
| Reamer Series & Substrate | Flute Geometry | Coating / Finish | Hole Tolerance Range | Target Workpiece Alloys | Seattle Industry Application |
|---|---|---|---|---|---|
| Solid Carbide HRC58-65 (0.4µm Ultra-Fine Grain) |
6-Flute Right-Hand Spiral / Left-Hand Cut | AlCrN / TiSiN Nanocoating | ISO H6 / H7 (±0.0025 mm) | Titanium Grade 5 (Ti-6Al-4V), Inconel 718, Stainless 15-5PH | Aerospace Jet Engine Mounts & Flight Control Valves (Renton Corridor) |
| Japan STK HSS-E / M42 Cobalt (8% Cobalt High-Speed Steel) |
Straight Flute / SP Spiral Flute | Bright Polished / TiN Coated | ISO H7 / H8 (±0.005 mm) | 7075-T6, 2024-T3 Aluminium, Low-Carbon Alloy Steels | Commercial Aircraft Airframe Sheet Metal & Rib Assemblies (Everett Hub) |
| Tungsten Carbide Tipped (TCT) (Brazed Steel Body) |
Multi-Flute Helical Step Geometry | DLC (Diamond-Like Carbon) | Custom Stepped Hole Sizes | CFRP Laminates, Metal Matrix Composites (MMC), Cast Iron | Next-Gen Structural Composite Panel Reaming & Space Hardware (Kent Valley) |
| DIN 206 / Hand & Machine Hybrid (High-Toughness Alloy Steel) |
Left-Hand Spiral / Square Drive Shank | Passivated Black Oxide / Bright | ISO H7 / H9 (±0.008 mm) | Bronze Sleeves, Marine Brass, 316 Stainless Steel | Shipyard Shaft Bushing Repair & Valve Rebuilding (Ballard & Port of Tacoma) |
Our chucking reamers are tailor-ground to overcome specific tooling bottlenecks encountered by Pacific Northwest CNC machinists and tooling engineers.
In the Everett and Renton aerospace manufacturing zones, precision pin-location holes in wing ribs, landing gear actuators, and fuselage stringers require strict H7 hole fitment with zero bell-mouthing. Our 6-flute solid carbide chucking reamers with unequal flute spacing eliminate chatter harmonics at speeds over 3,000 RPM, delivering consistent $Ra 0.2 \mu m$ finishes in stacked 7075-T6 aluminum and titanium structural joints.
Operations around Harbor Island, Ballard, and the Port of Tacoma demand heavy-duty chucking reamers capable of resizing worn marine bronze sleeves, rudder stock bushings, and hydraulic control valve bores. Our STK HSS-E straight-shank and square-head reamers resist chip welding and thermal distortion when reaming deep-hole bore features under flood coolant or MQL (Minimum Quantity Lubrication) systems.
Bellevue and Redmond’s burgeoning hardware incubators produce titanium surgical robotics components, clean-tech hydrogen fuel cell valves, and optical housing chassis. Using our custom micro-diameter chucking reamers (ranging from 1.5mm to 6.0mm), machine shops maintain exact press-fit alignments for micro-bearings and fluid seals without post-reaming deburring passes.
As manufacturing environments across Washington State digitize and automate, purchasing managers and shop leads are evaluating tooling vendors not just on upfront cost, but on holistic tool life, predictability, and semantic quality compliance:
Combining world-class German & Swiss grinding technology with rigorous QC standards to guarantee tool longevity and sub-micron repeatability.
Our production floor features ANCA TX7 and Walter Helitronic grinding centers running 24/7. Every chucking reamer profile—from straight flute to helical step designs—is ground using ultra-fine diamond wheels to achieve mirror-smooth flute surfaces and razor-sharp cutting edges.
Zero non-conforming tools leave our facility. Every production batch undergoes 100% automated optical inspection using Zoller Genius 3 measurement machines. We verify outer diameter tolerance, runout concentricity (< 0.002 mm), lip height, and rake angle before laser marking.
We maintain an optimized logistics channel specifically for Pacific Northwest clients. Urgent orders ship via DHL/FedEx Express direct to Sea-Tac airport (3-5 business days delivery), while high-volume stock orders ship via containerized sea freight to the Port of Seattle with all customs and import duty documentation pre-handled.
Answers to crucial compliance, tolerance, custom order, and delivery questions from our regional engineering technical desk.
Our H7 metric and equivalent fractional inch chucking reamers are manufactured in strict compliance with ISO 286-2 international standards, which match or exceed standard US aerospace tooling requirements (such as NAS 897 / Boeing D6 standards). Upon request, each shipment includes a certified CMM / Optical Inspection Report detailing outer diameter, shank runout, and pitch error.
Yes. Over 35% of our export volume to Washington State consists of custom tooling. You can send your STEP, IGES, or PDF engineering drawings directly to our engineering team. We supply a 3D tool simulation for approval within 24 hours and produce completed solid carbide or HSS-E step reamers within 7 to 10 working days.
For solid carbide chucking reamers with AlCrN coating cutting Titanium Grade 5, we recommend a surface speed ($V_c$) of 18 to 28 m/min (60–90 SFM) with a feed per tooth ($f_z$) of 0.03 mm to 0.08 mm depending on diameter. High-pressure flood coolant (minimum 20 bar) or internal oil mist (MQL) is essential to avoid thermal work-hardening on the hole wall.
We provide full DDP (Delivered Duty Paid) shipping terms for our clients in King, Snohomish, and Pierce counties. All customs clearance, US import tariffs, harbor maintenance fees, and final truck freight to your facility door are handled by our logistics forwarders—eliminating unexpected import surcharges for your accounts payable department.
For carbon fiber composites (CFRP) and glass-filled plastics, we utilize micro-grain tungsten carbide (0.4 µm grain size with 10% Cobalt binder) paired with Diamond-Like Carbon (DLC) or Chemical Vapor Deposition (CVD) diamond coatings. This provides an ultra-low friction coefficient (< 0.1) and prevents material edge buildup and fuzzing.
Standard metric H7/H8 chucking reamers listed in our catalog have no MOQ requirement (1 piece sample orders welcome). For custom drawing-based step reamers or special non-standard diameters, our standard MOQ is typically 5 to 10 pieces depending on complexity and raw material rod stock size.
Contact our engineering sales team today to request a factory-direct wholesale quote, request sample testing, or submit custom drawings for immediate quotation.
Inquire Now