
Explore our standard and custom-manufactured chucking reamers designed for CNC machining centers, automatic lathes, aerospace hole finishing, and heavy metallurgy tooling setups.
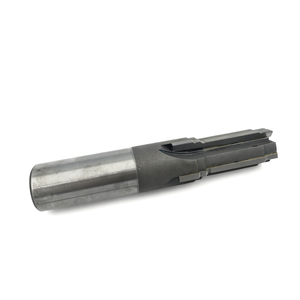
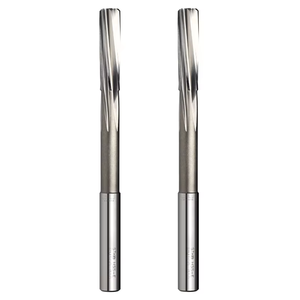
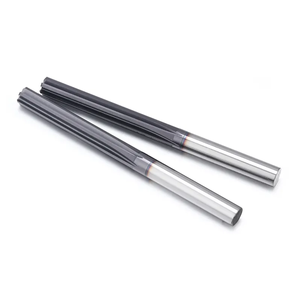
In high-precision manufacturing, drilling operations rarely achieve the dimensional stability, surface finish, and exact cylindricity demanded by aerospace, automotive transmission, hydraulic valve, and medical device assemblies. While a twist drill creates the initial cavity, it inevitably leaves micro-chatter marks, slight taper, and location drift. This is where chucking reamers serve as the ultimate hole-finishing instrument. Engineered with extremely tight back-taper tolerances, controlled chamfer lead angles, and unequalled radial runout precision, modern machine chucking reamers expand tool life while meeting strict ISO fit standards (H6, H7, H8, H9).
As a leading global chucking reamers factory and exporter, our production facility combines state-of-the-art 5-axis CNC Walter and ANCA grinders with premium sub-micron grain tungsten carbide and cobalt-enriched high-speed steels (HSS-E M35/M42). Whether sizing hydraulic manifold stepped bores or finishing fastener seats in carbon-fiber titanium composite stacks, selecting the optimal reamer geometry guarantees dimensional accuracy down to single-digit microns.
Utilizing micrograin tungsten carbide (0.6µm) with 10%-12% Cobalt content to maintain edge sharpness under high thermal friction and intense abrasive conditions.
Engineered back-taper geometry (0.001mm per 10mm) prevents heel rubbing, reduces frictional torque, and eliminates barrel-shaped or bell-mouthed holes.
Advanced TiAlN, AlCrN, and DLC coatings boost surface hardness up to HV 3300, allowing dry machining in cast iron and high-speed wet reaming in stainless steel.
Optimize speeds (SFM), feed rates (IPR), and flute geometries based on workpiece metallurgy and hole configuration.
| Workpiece Metallurgy | Recommended Material Substrate | Flute Configuration | Surface Speed (SFM) | Feed per Rev (IPR) | Coolant & Lubrication Strategy |
|---|---|---|---|---|---|
| Aluminium Alloys (2024 / 7075-T6) | Solid Carbide or Uncoated HSS-E | Straight Flute or LH Helix 45° | 120 - 250 SFM | 0.008" - 0.020" | High-pressure soluble oil mist or flood coolant |
| Austenitic Stainless (304 / 316L) | AlCrN-Coated Solid Carbide (HRC58+) | Left-Hand Helical / Right-Hand Cut | 35 - 75 SFM | 0.004" - 0.010" | EP (Extreme Pressure) synthetic oil emulsion |
| Titanium Alloys (Ti-6Al-4V) | M42 Cobalt HSS-E or TiAlN Carbide | Unequal Indexed 6-Flute Straight | 25 - 45 SFM | 0.003" - 0.007" | Flood coolant; continuous positive feed (never dwell) |
| Hardened Tool Steel (HRC 45-58) | Nano-Coated Ultra-Fine Carbide | Straight Flute with 45° Bevel Lead | 15 - 35 SFM | 0.002" - 0.005" | Micro-lubrication (MQL) or oil blast |
| CFRP / Composite Titanium Stacks | Diamond-Coated (CVD) Carbide | Dagger / Brad-Point Spiral Reamer | 150 - 300 SFM | 0.005" - 0.012" | Vacuum extraction with dry compressed air jet |
The global metalworking and tool manufacturing landscape is undergoing a structural transition driven by automation, electric vehicle (EV) component integration, aerospace lightweighting, and sustainable manufacturing mandates. Procurement executives and tooling engineers must align their supply chains with the following emerging industry trends:
With EV drivetrain manifolds, hydraulic control valves, and aerospace braking systems demanding multi-tiered concentric holes, purchasing single-pass stepped reamers has become a strategic priority. Rather than utilizing three distinct tool changes to process a counterbored valve seat, multi-flute stepped chucking reamers perform roughing, shoulder beveling, and final sizing in one continuous spindle downfeed, reducing cycle time by up to 65%.
Harmonic chatter is the leading cause of premature reamer wear and out-of-round holes. Modern tier-1 reamer factories are migrating toward variable-helix and uneven radial flute spacing (differential indexing). By disrupting periodic vibrational frequencies during cutting engagement, these tools deliver ultra-mirror surface finishes even on long-overhang setup configurations.
Tungsten and Cobalt remain critical raw materials with volatile global supply chains. Corporate sustainability goals (ESG) are driving high-volume buyers to mandate closed-loop tool recycling. Modern factory exporters now offer certified regrinding and recoating services that restore worn reamers to 98%+ of original factory performance at less than half the cost of new tooling purchase.
The standard straight shank with a flat drive is increasingly replaced by ultra-precision cylindrical shanks optimized for hydraulic expansion chucks and thermal shrink-fit holders. Achieving radial runout under 0.002mm at the tool point requires a seamless mechanical interface between the reamer shank and machine spindle toolholder.
Advanced high-speed reaming designs with optimized chamfer lead geometry allow machine operators to double their table feed rates while maintaining precise IT7 tolerance control. This evolution eliminates bottleneck operations in high-volume CNC automotive production lines.
Global procurement teams demand full compliance with international standards such as DIN 208, DIN 212, DIN 8093, and US aerospace specs (NAS 965 / NAS 937). Standardized shank metrics ensure seamless integration into international tool management systems.
Combining over three decades of aerospace tooling heritage with state-of-the-art CNC grinding technology, our facility provides global buyers with uncompromised tool quality, rapid custom manufacturing turnarounds, and rigorous quality assurance protocols.
Direct supplier status for government, defense, and Tier-1 aerospace contractors. Every batch is traceable back to raw material melt heats.
From fractional wire/letter sizes to metric H7 machine reamers, our warehouse maintains deep inventory depth to support immediate worldwide dispatch.
Need custom stepped diameters, specialized pilot guides, or unique helix angles? Our engineering team designs custom tooling drawings within 24 hours.
Answers to common engineering inquiries regarding chucking reamer selection, trouble-shooting, and global factory sourcing.
Straight flute chucking reamers are the industry standard for general-purpose through-holes and non-interrupted bores. However, when reaming holes containing keyways, cross-drilled oil ports, or internal splines, specify a Left-Hand Spiral / Right-Hand Cut reamer. The left-hand helix bridges internal gaps smoothly without tripping or tearing the hole edge while pushing chips forward out of through-holes.
Oversized or bell-mouthed holes usually stem from four primary issues: excess radial runout in the toolholder, spindle misalignment, excessive stock removal allowance, or a lack of back taper on the reamer. Ensure total indicator reading (TIR) at the reamer tip is under 0.005mm (0.0002"), utilize floating reamer holders for manual or turret lathes, and verify that pre-ream drill stock allowance is evenly distributed.
Solid carbide reamers offer exceptional rigidity, extreme thermal resistance, and long tool life in high-volume production setups running abrasive materials (cast iron, high-silicon aluminium, composites, hardened steels up to HRC 65). HSS-E (M35/M42 8% Cobalt) reamers provide superior toughness and flexural strength, making them far less prone to chipping in unstable machine setups, manual operations, or deep-hole hand reaming applications.
A standard H7 reamer is manufactured to cut within the upper and lower limits defined by ISO 286-2 for a specific nominal hole diameter. The reamer's actual OD is ground slightly above nominal size (e.g. +0.008mm to +0.012mm for a 10mm H7 hole) to account for natural material spring-back and initial wear allowance, ensuring the finished hole lands perfectly in the center of the H7 tolerance zone.
Yes. We specialize in custom OEM tool grinding. We fabricate specialized step reamers, pilot-guided reamers, extra-long reach shanks, and non-standard decimal diameters from 0.80mm up to 50.00mm within fast lead times. Simply send your part drawing or tool specifications through our live consultation service.
All tools are coated in anti-corrosion protective oil, encased in heavy-duty individual plastic tubes with tip protectors, and boxed in export-standard wooden or reinforced cartons. We ship globally via DHL, FedEx, air freight, and sea container freight, providing full COO (Certificate of Origin), MTR (Material Test Reports), and ISO calibration documentation.
Partner with an industry-leading chucking reamers factory. Our application engineers are available to review your workpiece drawings, recommend cutting parameters, and provide competitive factory-direct pricing.