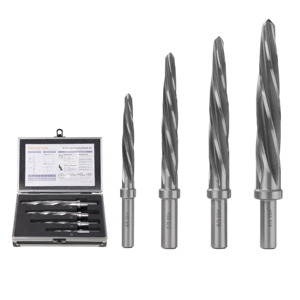
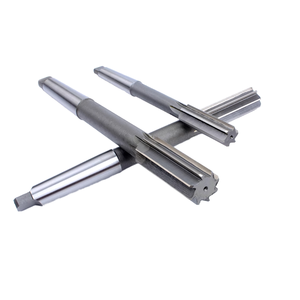
Engineered for high-rigidity CNC machining centers, specialized aerospace structural drilling, and manual precision chamber reaming. Explore our standard and custom-manufactured taper pin tooling options.
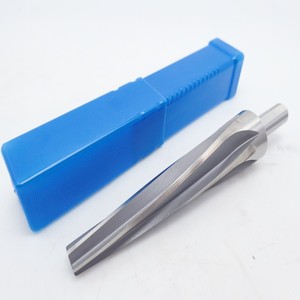
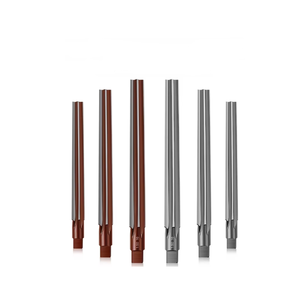
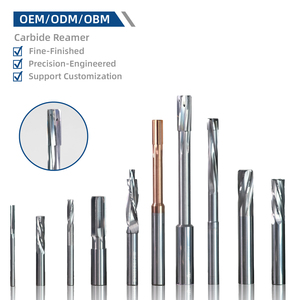
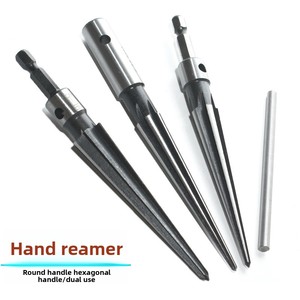
In modern sub-micron metalworking, aerostructure assembly, and high-duty mechanical joint fabrication, the accuracy of tapered holes dictates assembly alignment, shear-load capacity, and fatigue resistance.
The operational longevity of a taper reamer relies heavily on substrate selection. Standard high-speed steel (HSS M2) offers optimal toughness for manual taper pin insertion. However, for continuous high-speed CNC production on stainless steel or high-temperature superalloys (Inconel®, Titanium Ti-6Al-4V), premium Cobalt M35/M42 and ultrafine-grain Solid Tungsten Carbide (HRC 65-68) provide superior red hardness, mitigating thermal wear along the continuous cutting edge.
Taper reaming involves progressive cutting contact along the full axial length of the land, creating high radial forces prone to chatter. Utilizing Left-Hand Spiral, Right-Hand Cut flutes creates a forward pushing action on the chips, protecting blind hole bottoms while counteracting the tendency of the reamer to self-feed or wedge into soft non-ferrous metals like 2024/7075 aluminum.
We manufacture custom geometries spanning standard 1:50 Morse Tapers (DIN 208 / ISO 296), NMTB tapers, standard 7-degree spherical chamber reamers, and 10-degree conical aerospace profile tooling. Unequal flute spacing (variable index) is systematically ground to interrupt harmonic resonance frequencies during the final sizing pass.
As global industrial manufacturing accelerates toward Industry 4.0 automation, the global procurement model for precision rotary cutting tools is undergoing a fundamental transformation.
The aerospace industry's transition toward carbon-fiber-reinforced polymer (CFRP) composite skins bonded to titanium substructures requires specialized, single-pass dual-geometry taper reamers. Modern OEM buyers are bypassing off-the-shelf tools in favor of custom-engineered carbide reamers featuring DLC (Diamond-Like Carbon) or AlTiN nano-coatings to prevent composite delamination while maintaining clean hole diameter tolerances across multi-material interfaces.
Industrial buyers are moving away from multi-tier regional distributors toward direct relationships with OEM custom factories. Direct factory collaboration grants access to raw material heat-treatment certificates, 3D STEP cutting simulations, direct grinding wheel profile adjustments, and significantly reduced lead times for non-standard tooling setups.
Future automated CNC production lines demand tool shanks equipped with laser-etched DataMatrix codes or integrated micro-RFID tags. These systems automatically communicate run-out parameters, taper angles, tool life counters, and physical wear data directly to plant Manufacturing Execution Systems (MES), mitigating human setup errors during automatic tool changes.
Application parameters compiled by our OEM tooling engineers for optimizing cutting speed (SFM), feed rate, coolant delivery, and tool material configuration across key workpiece alloys.
| Workpiece Material | Recommended Substrate | Optimal Flute Geometry | Cutting Speed (SFM) | Feed per Tooth (IPT) | Recommended Coolant |
|---|---|---|---|---|---|
| Aluminium Alloys (2024 / 7075) | HSS M2 / Solid Carbide | 7°–10° Left-Hand Spiral | 150 – 250 SFM | 0.003" – 0.006" | Flood Mist / Soluble Oil |
| Austenitic Stainless Steel (304 / 316) | Cobalt M35 / Solid Carbide | Unequal Index Straight Flute | 40 – 70 SFM | 0.001" – 0.003" | High-Pressure Emulsion |
| Titanium Alloys (Ti-6Al-4V) | Micrograin Solid Carbide | Left-Hand Spiral 15° Helix | 25 – 45 SFM | 0.001" – 0.002" | Synthetic Flood Coolant |
| Cast Iron & Ductile Iron | Coated Carbide (AlTiN) | Straight Blade Groove | 80 – 120 SFM | 0.002" – 0.005" | Dry with Compressed Air |
| CFRP Composite Laminates | Diamond-Coated Carbide | Dagger Point Spiral Flute | 200 – 400 SFM | 0.002" – 0.004" | Vacuum Dust Extraction |
Achieving continuous sub-micron precision requires advanced 5-axis CNC grinding technology and automated micro-edge prep inspection protocols.
Utilizing ANCA and Walter 5-axis CNC grinding centers, flute indexing tolerances are maintained within ±0.001mm, ensuring equal chip load distribution across all teeth.
Controlled edge honing ($5\text{ to }15\text{ }\mu\text{m}$) eliminates micro-burrs and stress risers on the cutting lip, preventing sudden edge chipping under variable radial loads.
Advanced Physical Vapor Deposition (PVD) applies multi-layered AlTiN and TiSiN coatings to reduce coefficient of friction to below 0.3, reducing heat build-up during deep taper engagements.
100% of finished OEM lots undergo Zoller Genius non-contact optical inspection to verify taper angle fidelity, concentricity, radial runout, and surface finish metrics before shipment.
Over 35 years of dedicated manufacturing expertise, rigorous aerospace standards compliance, and worldwide engineering support make us a dependable direct supply partner.
Established under rigorous production frameworks (CAGE Code 0PFP1), our engineering facility adheres to National Aerospace Standards including NAS 965, NAS 907, NAS 937, and ISO quality management systems. We serve commercial airlines, third-party MRO stations, and military defense contractors globally.
Whether you require a short prototype run of 5 non-standard chamber reamers or volume contract production of 50,000 units, our flexible manufacturing lines deliver fast turnaround times (custom samples within 7–10 working days) with complete material traceability reports.
Our application engineering team provides direct consultative support to refine your tool geometry, select ideal shank configurations (ISO Taper, Morse Taper, Straight, or Hex Shank), and optimize CNC machine parameters to extend overall tool life and minimize per-hole tooling costs.
Answers to common technical queries submitted by tooling engineers, procurement specialists, and shop managers.
Straight flute taper reamers are ideal for general-purpose manual reaming and interrupted cuts where high rigidity is maintained. Left-hand spiral flutes with right-hand cutting action push chips ahead of the tool (away from the machine spindle), making them superior for blind-hole CNC applications, preventing tool clogging, and producing superior surface finishes ($Ra < 0.2\ \mu\text{m}$).
Solid Tungsten Carbide is recommended for high-volume automated CNC machining of abrasive or hardened materials (HRC > 35), such as stainless steel, heat-treated alloy steels, titanium, and carbon fiber composites. Cobalt HSS (M35/M42) is preferred in setups with lower rigidity, hand-held manual drilling operations, or thin-walled aircraft sheet metal assembly where tool flexibility prevents catastrophic tool breakage under slight misalignment.
Yes. As a direct custom OEM manufacturer, we produce custom taper angles ranging from sub-degree tapers up to extreme steep angles, conical spherical profiles, multi-step chamber reamers, and custom shanks (including Weldon flats, threaded shank NAS 965 Type D, ISO taper shanks, and quick-change hex shanks).
To combat radial chatter caused by continuous tooth contact, our engineering team utilizes unequal flute pitch spacing (variable indexing). Grinding flutes at slightly irregular angular intervals breaks up harmonic resonance during operation, stabilizing the cut and delivering circularity within micron-level tolerances.
We export globally via expedited air freight (DHL, FedEx, UPS) and sea freight with full export clearance documentation, CAGE code compliance, and commercial invoicing. Standard stock items ship within 24 hours; custom OEM production orders are completed in 7 to 15 business days depending on order complexity and coating requirements.
Need custom taper dimensions, specialized coating recommendations, or bulk export pricing? Connect directly with our tooling specialists for instant technical consultation and pricing support.