0%

Choosing Micro Stop Countersink Cages is a precision decision, not just a matter of matching a cutter diameter. The cage must fit the tool and workpiece, hold its setting under load, and produce a repeatable countersink without marking the surface. On a thin aluminum panel, even a small depth error can leave a visible ring or an uneven fastener seat. Small details matter.

For reliable selection, compare cage compatibility, adjustment range, locking method, bearing contact, and measured depth repeatability. ISO 230-1 addresses geometric accuracy testing for machine tools, while ASME Y14.5 provides principles for interpreting dimensional tolerances. Neither standard is a market report for this product category. I cannot verify a public industry data report or an attributable expert quotation specifically about Micro Stop Countersink Cages from the material available here, so inventing a statistic or expert quote would be misleading. Ask suppliers for test results and application references instead.

A useful evaluation is practical: set the cage, machine several test pieces, then measure the countersink depth and inspect the surface under good light. Record the results. Repeatability beats a polished claim. One caveat deserves attention: nominal adjustment increments do not guarantee the same performance across materials, operators, or setups. Choose Micro Stop Countersink Cages against the actual fastener, material, and production conditions—and verify the result before committing to a full run.
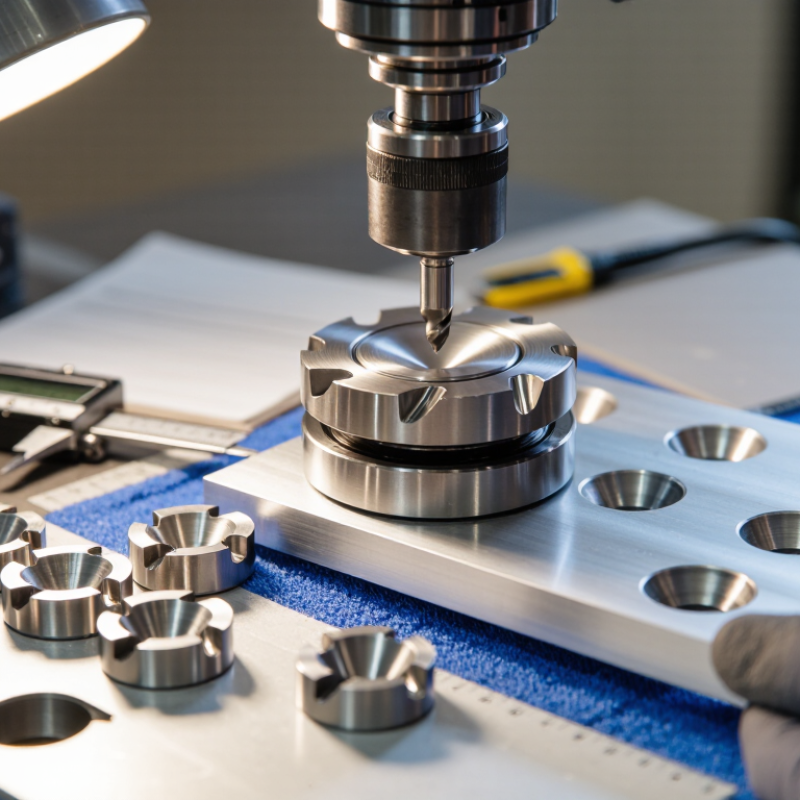
How to Choose Micro Stop Countersink Cages

Define the Micro-Stop Cage’s Role in Controlling Countersink Depth

A micro-stop cage is a mechanical depth limiter, not just a holder for the cutter. Its sleeve rests on the work surface while the spindle advances; the cage’s setting limits how far the countersink can enter. This matters because a few extra turns can leave a fastener head below the surface or thin the material around the hole. FAA Advisory Circular 43.13-1B discusses 100-degree flush-rivet geometry, a useful reference for understanding why cutter angle and seating depth must be treated separately. The angle describes the cone. The cage controls its depth.

Set the cage against a clean, flat test surface, then make a light cut in scrap of matching thickness. Measure the result with a depth gauge or check the actual fastener’s seating. A cage set by feel alone can drift, especially if its contact sleeve is dirty or the locknut loosens. Small details matter. Verify the setting after changing cutters, materials, or fasteners, and follow the engineering drawing’s tolerance rather than assuming every flush head needs the same cut. A slightly proud head may be deliberate. That is easy to overlook. The cage makes repeatable depth possible, but it cannot correct a tilted tool, a worn cutter, or an incorrect setup.

How a Micro-Stop Cage Controls Countersink Depth

With the tool geometry and reference surface held constant, adjusting the cage’s axial stop travel changes the nominal countersink depth. The chart shows an ideal 1:1 calibration relationship; actual results should be verified on a test piece.

Depth-to-diameter results also depend on countersink angle, cutter geometry, and the pilot-hole diameter. Use a consistent setup and check the finished depth before production.

Choose 82° or 100° Cutter Angles to Match Common Fastener Types

How to Choose Micro Stop Countersink Cages

Cutter angle must match the fastener head, not merely the material. ASME B18.6.3 specifies 82° flat-head machine screws, a common choice for general-purpose assemblies. NAS1097 identifies 100° reduced-head rivets used in aerospace applications. These standards show why an apparently small angle difference matters: a mismatched cutter can leave a visible rim, poor seating, or an oversized recess. Check the fastener’s governing specification before selecting a cage and cutter. Small mismatch, real consequences.

A micro-stop cage controls countersink depth; it does not correct the cutter angle. Fit the 82° or 100° cutter, then set the stop on a scrap coupon of the same material and thickness. A screw head should sit flush without rocking, while the surrounding surface stays intact. For thin aluminum, inspect both sides for distortion and verify the depth with the actual fastener. FAA AC 43.13-1B provides accepted aircraft inspection and workmanship guidance, but the applicable design specification takes precedence. I have seen a “close enough” setting pass a quick glance, then reveal a proud head under a straightedge. Recheck after changing cutters, since cage settings and tool runout can shift the result.

Check Cutter Shank, Cage Fit, and Runout Against Tooling Specifications

A micro stop countersink cage is only as accurate as its fit. Match the cutter’s shank diameter and usable length to the cage and holder specifications. Check that the cutter seats fully, without rocking or binding. Then confirm the cage’s depth-adjustment range suits the countersink and material thickness. A snug fit matters. But forcing a close-fitting shank into the cage can damage parts and compromise alignment.

Runout deserves a measured check, not a visual guess. With the cutter installed, rotate the spindle by hand and measure near the cutting end with a suitable indicator. ISO 230-7:2015 describes methods for measuring spindle error motion; it does not provide one universal runout limit for every setup. Use the allowable runout stated in the tooling specifications, and record the reading before production. Excessive runout can produce uneven cutting and a rough, oversized seat. One easy-to-miss detail: dirt on a mating surface can mimic poor fit.

Tips: Clean the shank and cage bore. Verify the shank diameter, seating depth, and cage adjustment against their drawings. If the reading changes after reseating, inspect for burrs or debris before changing the setup. A second check is worthwhile. Small assemblies can still surprise you.

Set Depth Using 0.001-Inch Graduations (0.0254 mm) and a Test Hole

Micro stop countersink cages help control depth, but their graduations work best with a consistent setup. Each 0.001-inch mark equals 0.0254 mm. That small step can change whether a fastener sits flush or stands proud. Use a sharp cutter and clamp the workpiece firmly. Keep the cage square to the surface. Set the scale near the desired depth, then lock the cage before cutting. Small changes matter.

Make a test hole in scrap with the same material and support as the finished part. Clear the chips, then check the countersink with the intended fastener or a depth gauge. A fastener that rocks or sits high may indicate insufficient depth; one that sinks below the surface has gone too far. Adjust by one graduation at a time, following the scale’s indicated direction, and cut another test hole. Don’t rely on the dial alone.

Surface variation can make a perfect-looking scale reading misleading. That is easy to overlook. Check the test hole under good light, and note the setting that gives a consistent fit. If the material, cutter, or work support changes, test again rather than assuming the old setting will transfer. Keep the workpiece secured whenever cutting, and stop the spindle before adjusting the cage.

Verify Countersink Size and Fastener Flushness Against the Part Drawing

How to Choose Micro Stop Countersink Cages

Verify Countersink Size and Fastener Flushness Against the Part Drawing

A micro-stop countersink cage is useful only when its setting matches the part drawing. Check the specified countersink diameter, included angle, and fastener head style before adjusting the stop. A small mismatch can leave the head proud or buried below the surface. Details matter.

Measure a representative countersink with suitable inspection tools, then compare the result with the drawing’s tolerance and datum. Do not rely on visual flushness alone. A fingernail may catch a slight step, but it cannot confirm diameter or angle. Test the fastener in the actual part, or in a matching coupon when production parts are limited. Confirm that the head sits flush without rocking.

After setting the cage, make a trial cut and inspect both the countersink and the installed fastener. Check twice. Recheck after tool changes, cage adjustments, or noticeable wear. Material thickness and burrs can affect seating, even when the depth setting seems unchanged.

A clean-looking result can still miss the specified size; that is easy to overlook. Record measurements and setup details so another operator can repeat the check. If the drawing is unclear, resolve the requirement rather than guessing at flushness.

FAQS

What does one graduation on a micro-stop countersink cage represent?

Each 0.001-inch mark equals 0.0254 mm. Small changes can affect whether a fastener sits flush.

How should I set the cage before cutting?

Use a sharp cutter and secure the workpiece. Keep the cage square, set the scale near the target, then lock it. Stop the spindle before adjusting.

Why should I make a test hole?

A test hole in matching scrap helps confirm the setting before cutting the finished part. Use the same material and support. Don’t trust the dial alone.

How can I check whether a fastener sits correctly?

Try the intended fastener in the test hole. It should sit flush without rocking. A high head may mean the cut is too shallow; a buried head may mean it is too deep.

How should I adjust the countersink depth?

Change the setting by one graduation at a time, following the scale’s direction. Cut and inspect another test hole. Small steps matter.

What details should I check on the part drawing?

Confirm the countersink diameter, included angle, fastener head style, tolerance, and datum. Flushness alone does not verify size or angle.

Can I rely on visual inspection to confirm the countersink?

No. Good lighting helps, and a fingernail may catch a raised edge. Use suitable inspection tools and compare measurements with the drawing.

When should I repeat the test cut?

Test again if the material, cutter, or work support changes. Recheck after cage adjustments or noticeable cutter wear. I might overlook a small change, too.

What setup details should I record?

Record the cage setting, measurements, material, and support conditions. These notes help another operator repeat the check. A clean finish can still be out of specification.

Conclusion

Micro Stop Countersink Cages help control how deeply a countersink is cut, supporting consistent results across a part or production run. Choose a cutter angle that matches the fastener design: 82° and 100° are common options, but the part drawing and fastener specifications should guide the choice. Before cutting, confirm that the cutter shank and cage fit the tooling correctly, and check for excessive runout that could affect accuracy or surface quality.

Set the cage depth with its 0.001-inch (0.0254 mm) graduations, then make a test hole in suitable material and inspect the result. Measure the countersink and check that the fastener sits flush as required by the drawing. If the fit or depth is off, adjust the setting and test again before working on the part. This careful process helps achieve repeatable countersinks while reducing the chance of rework.
Clara

Clara

Clara is a seasoned marketing professional with a strong understanding of customer needs, market trends, and the practical value of innovative business solutions. As a key contributor to the company’s content and communication strategy, she regularly updates the company website with insightful blog......