0%

Chatterless Countersinks are designed to reduce vibration and leave cleaner, more consistent chamfers. In practice, the result depends on more than the cutter. Material, spindle speed, feed rate, tool condition, and workholding all matter. A countersink that runs smoothly in aluminum may behave differently in stainless steel or a thin sheet. Small changes can show up as ripples around the hole.

A clean edge matters. So does repeatability. But the word “chatterless” can sound more certain than shop reality allows. That deserves a pause. No tool can compensate for every setup problem, and product claims should be checked against the job at hand. Shank size, included angle, cutting material, coating, and flute design are practical details worth comparing before purchase.

This guide presents seven tips for choosing Chatterless Countersinks with your actual work in mind. It covers how to match the countersink to the base material and hole size, assess construction and geometry, and consider machine compatibility. It also highlights signs of poor fit, such as rough edges, uneven seating, or repeated chatter marks. These clues may point to the tool, the setup, or both. A short test cut can reveal more than a polished product description. Check specifications, inspect sample results, and consider how often the tool will be used. The best choice is not always the most expensive one. It is the one that performs reliably in your conditions.
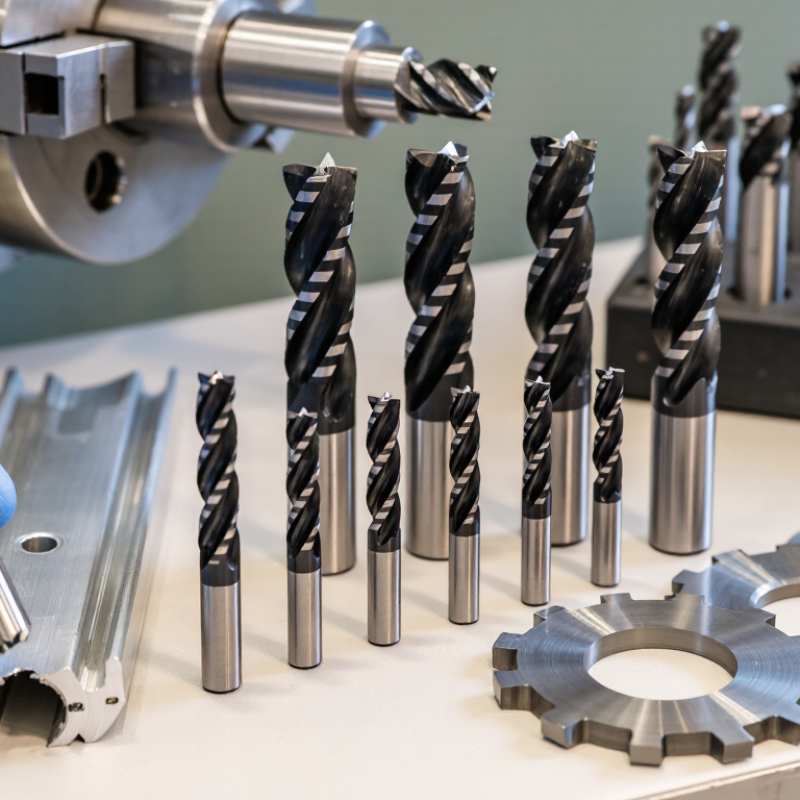
7 Tips for Buying Chatterless Countersinks

Understanding Chatterless Countersinks and How They Reduce Vibration

A countersink cuts a cone-shaped recess around a drilled hole, often to seat a flat-head screw or remove a sharp edge. Chatter appears as vibration, leaving ripples or a rough, uneven finish. A chatter-reducing design aims to make cutting forces steadier. Some tools use uneven flute spacing or specialized cutting-edge geometry to interrupt repeating vibration. The exact design varies, so check the tool’s specifications rather than assuming every countersink works the same way.

Setup matters just as much. Keep the workpiece firmly clamped, use a suitable pilot hole, and avoid excessive tool overhang. A loose part can buzz against the table. So can a worn spindle or a tool with runout. It is easy to blame the cutter. That is not always fair. I have seen a small change in clamping improve a finish more than swapping tools.

Choose a countersink suited to the material and hole size, then follow its recommended speed and feed guidance. If the cut squeals or leaves regular rings, stop and inspect the setup, edge condition, and alignment. A light, controlled cut often produces a cleaner bevel than forcing the tool. Still, results depend on the machine, material, and operator; “chatterless” does not mean vibration is impossible.

Matching Countersink Material and Geometry to the Workpiece

Chatterless countersinking starts with the workpiece, not the catalog. In aluminum, a sharp cutter and open flute space help clear gummy chips. In stainless steel, use a rigid setup and a wear-resistant edge; rubbing from a dull cutter quickly raises heat and can leave a torn rim. Plastics need light pressure and a keen edge, since excess heat can melt the lip. Small detail. Match the included angle to the fastener drawing, then check the seat with the actual screw. ISO 15065:2005 specifies 90-degree countersinks for certain metric countersunk screws; inch-based hardware may require 82 degrees. A mismatch can leave the screw head standing proud or bearing only at its edge.

Choose material for both the workpiece and the job. Carbide often keeps its edge longer in abrasive materials and repeated production, while high-speed steel can be less brittle and easier to resharpen for occasional use. The U.S. Geological Survey’s Mineral Commodity Summaries 2024 estimated global tungsten mine production at 78,000 metric tons in 2023. That signals tungsten’s industrial scale, not that carbide suits every cut. Clamp the workpiece, check spindle runout, and test on scrap. Listen for a steady cutting sound, not a pulsing squeal. Geometry may be correct; the setup may not be.

7 Tips for Buying Chatterless Countersinks — Matching Countersink Material and Geometry to the Workpiece

Tip Workpiece or requirement Countersink material to consider Geometry and buying guidance Why it helps reduce chatter
1. Match the included angle to the fastener. Flat-head screws and other countersunk fasteners; angle requirements vary by fastener standard and application. Choose HSS, cobalt HSS, or carbide according to the workpiece and production conditions; angle selection is independent of tool material. Common included angles include 82°, 90°, 100°, and 120°. Check the fastener specification and confirm the required seat with a sample part rather than assuming one angle fits all. A correctly matched seat supports the fastener head evenly and avoids forcing the tool to cut an unsuitable profile.
2. Choose a sharp, suitable tool for aluminum. Aluminum and other relatively soft, ductile nonferrous metals. Sharp HSS or carbide designed for nonferrous materials; a suitable low-friction coating may help, but coating choice should follow the tool maker’s guidance. Look for a polished cutting surface and geometry intended to clear soft, continuous chips. Keep the tool sharp and prevent chips from packing into the cutting area. Built-up material on the cutting edge can make cutting uneven and promote vibration or a rough, scored countersink.
3. Account for work hardening in stainless steel. Austenitic stainless steels and other grades that can work-harden during cutting. Cobalt HSS is a common choice for added hot-hardness; carbide may suit rigid setups and higher-volume work. Use a sharp tool and a stable feed. Avoid dwelling or rubbing at the hole edge; select the cutting geometry and operating parameters recommended for the specific stainless grade. Rubbing can harden the surface locally, increasing cutting forces and encouraging the tool to vibrate or wander.
4. Scale tool hardness to steel and production demands. Carbon and alloy steels, with hardness and production volume considered. HSS can suit general-purpose work; cobalt HSS offers greater hot-hardness; carbide is often selected for harder materials or production on a rigid machine. For a handheld drill or a less rigid setup, prioritize a robust, sharp tool and secure workholding. Use carbide only where the machine, holder, and setup can support its greater sensitivity to impact and misalignment. A tool that is too brittle for a flexible setup can chip; a dull or unsuitable tool can require higher force and aggravate vibration.
5. Use low cutting pressure on plastics. Thermoplastics and other heat-sensitive plastics. Sharp HSS or a tool specifically intended for plastics; keep the cutting edge clean and undamaged. Choose geometry that cuts cleanly rather than rubbing, and follow the plastic supplier’s recommendations. Test on a sample because plastics vary in stiffness, heat sensitivity, and tendency to chip or melt. Excessive friction can soften or melt plastic, while a grabbing cut can crack or deform the workpiece.
6. Support composite laminates and control edge breakout. Fiber-reinforced laminates and layered composite panels. Carbide or diamond-coated tooling may be appropriate for abrasive fiber reinforcement; select a tool specified for the particular composite. Use a geometry designed for composite countersinking, support the laminate where practical, and verify the result on a representative sample. Composite dust requires suitable extraction and protective measures. Abrasive fibers can wear ordinary edges quickly; wear and unsupported layers can contribute to rough cuts, delamination, or vibration.
7. Select flute and shank features for the setup. Any material, especially when chatter or inconsistent finish has been a recurring issue. Choose the cutting material for the workpiece first, then select a compatible countersink design and holder. Single-edge or purpose-designed chatter-reducing styles can be useful in some applications, but no flute design eliminates poor setup. Check shank fit, runout, tool overhang, workholding, and the manufacturer’s recommended cutting data. Secure clamping, low runout, short overhang, and a stable feed reduce the vibration sources that geometry alone cannot correct.

Note: These are general selection guidelines, not universal cutting parameters. Workpiece grade, hardness, hole size, machine rigidity, and tool design all affect performance; consult the tool and material suppliers for application-specific recommendations.

Checking Shank, Tool Size, and Machine Compatibility

7 Tips for Buying Chatterless Countersinks

Checking Shank, Tool Size, and Machine Compatibility

A quiet cut starts with a secure shank. Match its diameter and shape to the collet or chuck, then check the holder’s stated capacity. A loose fit can amplify vibration; a shank that barely enters is not a safe workaround. Inspect the mating surfaces for chips and wear. Tiny marks matter.

Tool size must suit both the hole and the machine. Compare the countersink’s cutting diameter and included angle with the fastener head and workpiece material. Then check the spindle’s speed range and the holder’s limits.

The U.S. Cutting Tool Institute and AMT reported roughly $2.6 billion in U.S. cutting-tool consumption in 2023, reflecting how much production depends on correctly selected tooling. That figure covers a broad tool market, not countersinks alone. Still, fit deserves attention.

Before production, check the machine manual for holder compatibility and maximum speed. If the tool has a long overhang, expect more chatter risk; reduce it where practical. A short test cut in scrap can reveal a poor match early. Listen, but inspect the countersink finish too. A smooth sound can mislead. One detail is easy to miss: runout. Measure it at the tool tip when possible, and recheck after tightening.

Evaluating Coatings, Build Quality, and Expected Tool Life

A quiet countersink starts with a coating matched to the job, not the hardest coating on the shelf. For abrasive materials, a wear-resistant coating can slow edge rounding; for softer metals, a sharp, polished cutting edge may matter more than added hardness. Check the maker’s stated substrate, coating type, and recommended speed range. Those details are more useful than a vague “long-life” claim. A dark coating can hide early wear, so inspect the cutting edge under bright light.

Tip: Compare build quality at the cutting lips. They should meet evenly, with no chipped corners or visible burrs. A rigid shank and concentric body help limit vibration; even slight runout can leave a ring of chatter marks. I still check the first hole twice. It takes a moment, but saves guesswork later.

Estimate tool life using a repeatable test: same material, speed, feed, and hole count, then inspect the edge and finish. ISO 3685:1993 gives 0.3 mm average flank wear as a common tool-life criterion for carbide turning tests. That figure is not a countersink limit, but it shows why wear needs a defined measurement. Track the number of clean holes before chatter or roughness appears, and record the result by material and coating. Expect variation; setup rigidity and chip evacuation can change the outcome more than the coating alone.

Comparing Performance, Cost, and Supplier Support Before Buying

Compare chatterless countersinks under the conditions you actually use. Keep the workpiece material, hole size, machine, and cutting settings consistent. Inspect the countersink edges for chatter marks, burrs, and uneven finishes. A smooth first cut is useful, but repeatability across several holes matters more. Small differences matter. Record tool life and any changes in cycle time; a quiet cut alone does not prove better performance.

Price each tool against its useful life, not just its purchase cost. Include replacement frequency, regrinding options, rejected parts, and time spent adjusting the setup. A lower-priced countersink may cost more if it leaves rough edges or needs frequent replacement. Still, shop conditions vary, and estimates can be wrong. A small, controlled trial can reveal costs that a catalogue cannot.

Supplier support also affects the decision. Ask for clear guidance on suitable materials, operating conditions, and maintenance, along with written specifications. If possible, request a sample or a technical review of your application before ordering in quantity. Notice how quickly the supplier answers specific questions, and whether the advice acknowledges limitations. That takes time. A helpful response is valuable, but verify recommendations on your own equipment before standardizing the tool.

FAQS

What is a chatterless countersink?

It is designed to reduce repeating vibration while cutting a cone-shaped recess around a drilled hole. “Chatterless” does not mean vibration is impossible.

What causes chatter during countersinking?

Vibration can come from cutting forces, a loose workpiece, tool runout, or a worn spindle. The cutter is not always to blame.

How can I reduce chatter with my current setup?

Clamp the workpiece firmly, use a suitable pilot hole, and limit tool overhang. Even a small change in clamping can improve the finish.

What signs suggest chatter during a cut?

Listen for squealing and inspect the bevel for regular rings or rough marks. Stop and check the setup before continuing.

How should I choose speed and feed settings?

Match the countersink to the material and hole size, then follow its recommended settings. Avoid forcing the tool; a light cut may leave a cleaner bevel.

How can I compare countersinks fairly?

Keep the material, hole size, machine, and settings consistent. Check several holes for chatter marks, burrs, and uneven finishes. One smooth cut proves little.

Is a lower purchase price always better?

No. Compare useful life, replacement frequency, regrinding options, rejected parts, and setup time. Estimates can be wrong, so test on a small scale.

What should I ask a supplier before buying?

Request written specifications and guidance for your material and operating conditions. Ask about maintenance, sample testing, and application review. Then verify the advice on your own machine.

Conclusion

Chatterless Countersinks are designed to reduce vibration and chatter, helping create smoother, more consistent countersinks. Before buying, consider the workpiece material and choose a cutter material and geometry suited to it. The right combination can improve cutting stability, surface finish, and tool performance across different applications.

Check that the shank, cutter size, and overall dimensions are compatible with your machine and setup. Compare coatings and build quality, since these can affect wear resistance and expected tool life. Finally, weigh cutting performance against purchase and replacement costs, and consider whether the supplier offers clear product information and dependable support. By evaluating these factors together, you can select a countersink that fits your machining needs and provides reliable value over time.
Ethan

Ethan

Ethan is a professional marketing specialist with a deep understanding of the company’s products, customers, and industry environment. Through a combination of market insight, strategic thinking, and clear communication, he helps present the company’s value in a practical and engaging way. Ethan......