0%

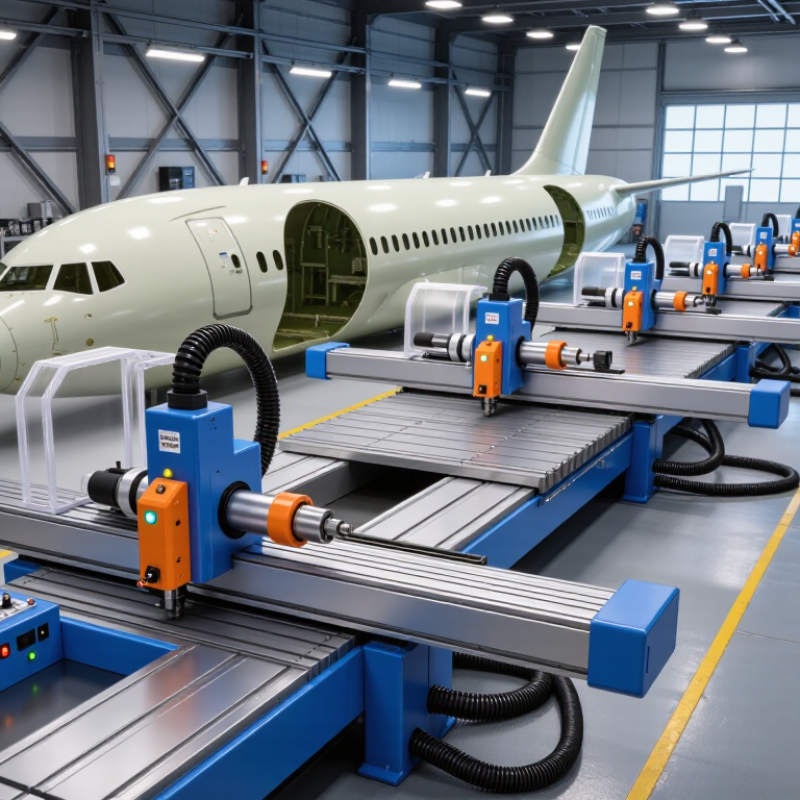
Choosing the 2026 best Aircraft Taper Routers requires more than comparing spindle speed or purchase price. Global buyers need dependable cutting accuracy, controlled dust extraction, and service support near production sites. A router may appear powerful on paper, yet perform poorly when machining curved composite panels or narrow aircraft taper sections.

Industry demand gives this decision greater importance. Boeing’s Commercial Market Outlook 2024 forecasts 43,975 new commercial aircraft deliveries over the next 20 years, representing approximately $7.2 trillion in market value. Airbus’s Global Market Forecast also identifies sustained demand for new aircraft and aftermarket services through 2044. These projections suggest continuing pressure on suppliers to improve repeatability, throughput, and production flexibility.

This guide evaluates Aircraft Taper Routers through practical manufacturing criteria. These include positional accuracy, five-axis capability, tool-change reliability, software compatibility, operator safety, and lifecycle support. The review also considers aerospace quality expectations linked to AS9100D, along with traceable maintenance records and documented calibration procedures. Those details matter beside a composite skin, where a small edge defect can create rework, delay, or material waste.

No ranking is perfectly universal. Facility layout, material type, regional voltage, and technician availability can change the best choice. Some supplier claims are difficult to compare directly. Therefore, buyers should request sample cuts, verified accuracy data, noise measurements, and references from comparable aerospace workshops. The strongest machine is not always the fastest one. It is the router that remains predictable after months of demanding production.
2026 Best Aircraft Taper Routers for Global Buyers?

Aircraft Taper Routers: Definition, Purpose, and Main Applications

Aircraft Taper Routers: Definition, Purpose, and Main Applications

An aircraft taper router is a precision cutting tool designed to create controlled tapered holes or openings. Its cutter gradually widens the hole instead of removing material at one fixed diameter. This shape supports tapered fasteners, bushings, and fitted components used in airframe assembly and maintenance. The tool may operate pneumatically or electrically, depending on the work area and required control.

Purpose and Precision

Its main purpose is dimensional accuracy. A technician can set the cutting depth, guide the router along a marked center, and produce a consistent taper in aluminum, composite panels, or approved lightweight structures.

Surface Quality and Control

Clean edges matter. Rough surfaces may increase stress, weaken fastener seating, or hide delamination around composite holes. Practical users check tool runout, cutter sharpness, and hole alignment before cutting. A small error can become expensive.

Common Applications

Common applications include repairing skin panels, preparing structural joints, enlarging existing holes, and fitting tapered inserts. Some routers use depth stops or interchangeable cutters for different angles. However, these features do not replace inspection. Material thickness, fiber direction, and heat buildup can change the result. I have found that speed alone is a poor measure of performance. A slower pass often produces a cleaner surface, though this depends on cutter condition and operator control. Maintenance records, calibration checks, and approved technical procedures remain essential for reliable aircraft work.

Aircraft Taper Router Types and Their Material Compatibility

2026 Best Aircraft Taper Routers for Global Buyers?

Aircraft Taper Router Types and Their Material Compatibility

Aircraft taper routers are selected by geometry, cutting edge, and workpiece behavior. Common types include single-flute routers, multi-flute cutters, and abrasive-coated tools. Single-flute designs clear chips efficiently in aluminum and reduce heat during controlled trimming. Multi-flute cutters can improve surface finish on stable metal parts. They need careful feed control. Abrasive-coated tools suit glass-fiber and carbon-fiber laminates, where sharp metal edges may cause fraying.

Carbide cutters generally handle aluminum, mild steel, and some titanium applications. Titanium demands slower cutting conditions and strong heat control. High-speed steel may work for softer metals, but it often loses hardness sooner. Diamond-coated or polycrystalline cutting edges can perform well on composite panels and honeycomb skins. They are not automatically suitable for every metal. Resin content, fiber direction, panel thickness, and clamping pressure all change tool life.

Match the taper angle, cutting diameter, and shank size before machining. A six-degree taper is not interchangeable with a ten-degree taper. Check the router’s chip clearance against the material’s dust and chip behavior. Use an offcut when possible. I have found that a perfect material chart does not exist. Real panels can contain voids, cured resin pockets, or uneven support. A clean first pass may still hide heat damage underneath. Inspect edges with magnification, measure the final taper, and adjust feed rates gradually. Fancy tooling cannot correct poor fixture control.

Key Specifications for Comparing the Best 2026 Models

For global buyers, an aircraft taper router should be compared through measurable specifications, not advertised cutting speed. Check spindle speed, motor power, collet range, taper-angle control, feed rate, and positional repeatability. A practical baseline is a variable spindle range near 10,000–30,000 rpm, with repeatability below 0.05 mm for controlled composite trimming. Higher speed is not always better. Excessive heat can soften resin and damage a clean edge.

The 2024 International Air Transport Association report recorded global passenger demand above 2019 levels, increasing pressure on maintenance capacity and turnaround time. The 2024 aerospace and defense industry outlook from Deloitte also highlights production efficiency and supply-chain resilience.

Therefore, buyers should examine cycle-time data, extraction performance, noise levels, and service access. A router with 2.2–3.0 kW power may handle common composite panels, but thick laminates require testing with the actual cutter and material. Do not trust a brochure alone.

For workshop reliability, inspect calibration records, emergency-stop design, dust containment, and compatibility with local electrical standards. A sealed linear guide is valuable in dusty environments. A five-axis option can reduce repositioning, yet it adds setup complexity and training demands. In my experience, operators often underrate ergonomics; a heavy head creates small errors after repeated passes. The best comparison includes a witnessed trial, measured surface temperature, edge quality, and tool wear. Specifications can still mislead.

Global Buying Factors: Safety, Standards, Supply, and Total Cost

2026 Best Aircraft Taper Routers for Global Buyers?

Buying an aircraft taper router requires more than comparing spindle speed and purchase price. Safety should guide the shortlist. Look for enclosed cutting areas, reliable emergency stops, stable workholding, and effective dust extraction. Operators also need clear training materials and guarded access points. A quiet machine is helpful, but measured noise data matters more than sales language.

Standards must match the destination market. Request electrical conformity documents, risk assessments, factory test records, and calibration reports. Verify whether certificates cover the complete machine, not only individual components. Traceable serial numbers and documented maintenance procedures improve accountability. Some suppliers provide impressive files, yet their technical translations remain weak. That deserves careful questioning.

Supply reliability affects production almost as much as machine quality. Check lead times, spare-part availability, remote diagnostics, installation support, and local service capacity. Ask how quickly a replacement spindle or control board can arrive. Calculate total cost using freight, import duties, commissioning, tooling, training, energy use, calibration, and expected downtime. The cheapest quote may become expensive after one missed production week. A useful comparison table should show five-year ownership costs, not only the invoice amount. I would also request references from buyers operating in similar climates and regulatory environments. This step can feel slow, but it often reveals practical problems hidden during demonstrations.

2026 Best Aircraft Taper Routers for Global Buyers? - Global Buying Factors: Safety, Standards, Supply, and Total Cost
The comparison below uses common aircraft-composite and light-alloy taper-routing configurations. Values are indicative market ranges for procurement planning and must be verified against the final tool configuration, material specification, and destination-country requirements.
Buying Dimension Compact Pneumatic Taper Router Compact Electric Taper Router High-Speed Composite Router Right-Angle Taper Router Industrial Collet Router
Typical aircraft application Portable edge tapering, local repairs, and work near fuel-free maintenance areas Workshop tapering of composite panels, honeycomb skins, and light-alloy parts High-quality trimming of carbon-fiber, glass-fiber, aramid, and sandwich structures Access-restricted areas, curved surfaces, ribs, frames, and close-clearance assemblies Repeated production tapering, fixture-mounted work, and high-volume component preparation
Drive type Compressed-air vane or turbine motor Brushed or brushless electric motor High-speed electric motor, usually brushless Pneumatic or electric right-angle drive Industrial electric motor or external spindle system
Typical no-load speed 18,000–30,000 rpm 20,000–30,000 rpm 24,000–40,000 rpm 15,000–28,000 rpm 18,000–35,000 rpm
Typical rated input 0.35–0.75 kW pneumatic equivalent 0.60–1.20 kW 0.80–1.50 kW 0.40–1.00 kW 1.00–2.20 kW
Common collet sizes 3 mm, 6 mm, and 1/4 in 6 mm and 1/4 in; 8 mm on larger models 6 mm and 1/4 in; precision 3 mm options available 3 mm, 6 mm, and 1/4 in 6 mm, 8 mm, 1/4 in, and 3/8 in
Typical tool mass 0.70–1.40 kg 1.20–2.40 kg 1.00–2.00 kg 0.90–2.20 kg 2.00–5.00 kg
Speed-control method Air regulator, throttle lever, or built-in governor Electronic speed control; verify compatibility with the local power supply Electronic speed control with overload or temperature protection Air regulator or electronic control depending on configuration Variable-frequency drive or industrial electronic controller
Dust and chip management External extraction is normally required; compressed air must not disperse composite dust into the work zone Extraction shroud and conductive hose are recommended for composite dust Best suited to sealed shrouds, local extraction, and HEPA-rated filtration Extraction design depends on the restricted-access geometry Suitable for fixed extraction systems and controlled production cells
Operator safety priorities Low vibration, guarded trigger, hose restraint, and controlled exhaust direction Double insulation or protective grounding, spindle lock, thermal protection, and guarded switch Dust containment, anti-static extraction, low runout, overload protection, and emergency isolation Guard clearance, reaction torque control, and ergonomic access to confined areas Interlocked guarding, emergency stop, fixture stability, and documented maintenance procedures
Relevant standards and conformity checks ISO 12100 risk assessment; applicable ISO 11148 requirements for non-electric hand tools; local machinery and workplace rules ISO 12100; IEC 62841-2-17 for hand-held routers where applicable; IEC 60204-1 for integrated machinery ISO 12100; IEC 62841-2-17 where applicable; electromagnetic compatibility and dust-control requirements ISO 12100; applicable pneumatic or electric hand-tool requirements; regional conformity assessment ISO 12100; IEC 60204-1 for machinery electrical systems; guarding, control-system, and emergency-stop validation
Global electrical compatibility Generally favorable because the motor is air-powered; compressor voltage and local plant standards still require review Specify 100–120 V or 220–240 V and 50/60 Hz before purchase Specify voltage, frequency, plug, controller, and EMC configuration before shipment Air-powered versions simplify regional deployment; electric versions require the same voltage review as standard electric tools Usually requires site-specific electrical engineering and commissioning
Compressed-air requirement Typically 0.35–0.65 m³/min at approximately 6.0–6.3 bar Not required Not required unless an air-assisted dust or cooling system is specified Typically 0.30–0.60 m³/min at approximately 6.0–6.3 bar for pneumatic versions Not normally required for electric spindle configurations
Expected maintenance focus Air filtration, lubrication where specified, vane or bearing inspection, and hose-condition checks Carbon brushes if fitted, bearings, switch, cord, cooling passages, and extraction shroud Bearings, collet accuracy, cooling path, electronics, and dust-seal condition Gearbox or angle-head lubrication, bearings, and access-area guard condition Spindle bearings, collet runout, controller, guarding, fixture alignment, and extraction system
Indicative purchase price, USD $350–$1,200 $450–$1,600 $900–$3,000 $600–$2,200 $2,000–$8,000+
Typical planning lead time 2–8 weeks for standard configurations; longer for special collets or documentation packages 2–8 weeks for standard voltage and plug configurations 4–12 weeks when extraction, controller, or aerospace documentation is customized 4–12 weeks depending on angle-head geometry and tooling 8–20 weeks when fixtures, controls, and site acceptance testing are included
Estimated landed-cost exposure Purchase price plus approximately 15–35% for freight, insurance, import charges, and commissioning Purchase price plus approximately 15–35%; voltage conversion or replacement is not recommended as a substitute for correct specification Purchase price plus approximately 20–40% because of extraction, documentation, and validation requirements Purchase price plus approximately 20–40% depending on configuration and export documentation Purchase price plus approximately 25–50% for installation, controls, fixtures, training, and acceptance testing
Best global-buying advantage Low electrical complexity and good portability Simple workshop deployment and broad availability High process control for composite materials and dust-sensitive work Excellent access in restricted geometries Highest repeatability and productivity in controlled production
Main purchasing risk Insufficient compressor capacity, poor air quality, and uncontrolled composite dust Incorrect voltage, inadequate extraction, and unsuitable cutter speed for the laminate Higher total cost if dust extraction and validation are excluded from the quotation Restricted tool access can reduce visibility and increase setup time High initial cost and longer integration time if the workholding system is not defined
Recommended buyer profile Maintenance teams and mobile repair operations with a reliable compressed-air network Small and medium workshops requiring flexible general-purpose taper routing Composite-focused facilities prioritizing surface quality and dust control Manufacturers working on complex airframe geometry or confined spaces Production facilities seeking repeatable output, digital controls, and documented process capability

Selection rule: For most global buyers, the best choice is not the highest-speed router. It is the configuration that matches the material, cutter diameter, required taper angle, extraction system, local power or air supply, and documented safety controls.

Safety note: Carbon-fiber, glass-fiber, aramid, and metal dust can present inhalation, skin, electrical, or fire risks. Use a validated extraction system, suitable respiratory and eye protection, grounding or anti-static measures where required, and a documented risk assessment.

Standards note: CE, UKCA, or other conformity markings are not substitutes for checking the complete technical file, declaration of conformity, operating instructions, guarding, electrical rating, EMC documentation, and destination-country import requirements.

Total-cost note: Landed cost should include the tool, collets, cutters, extraction equipment, compressor capacity where applicable, freight, insurance, duties, taxes, spare parts, training, calibration, and commissioning.

Indicative ranges are procurement-planning estimates for 2026 and are not quotations or certification claims for any specific product.

How to Select, Use, and Maintain an Aircraft Taper Router

Selecting an aircraft taper router starts with the joint, material, and required taper angle. Check the cutter range, spindle speed, collet accuracy, and feed control before comparing prices. A stable base matters when working near thin skins or curved panels. The tool should feel balanced, not merely powerful. Verify electrical compatibility, documentation, replacement parts, and service support for your region. These details often decide long-term value.

Tips: Test the router on scrap material first. Mark the cut line clearly. Use sharp, approved cutters and secure the workpiece firmly. Wear eye and hearing protection, then keep loose clothing away from the spindle. Let the tool reach full speed before contact. Never force the feed. Small passes usually produce cleaner edges and reduce heat.

During use, inspect the taper after every few passes. Measure depth with a calibrated gauge instead of relying on appearance. Dust, chips, and vibration can hide a poor cut. Maintenance should include cleaning the collet, checking the base, and inspecting cables or air lines. Store cutters dry and protected from impact. Even experienced users can overlook gradual vibration. That mistake deserves attention. Replace damaged components through qualified service channels, and follow the tool’s technical manual for torque, lubrication, and inspection intervals. A short maintenance record can reveal patterns before they become expensive problems.

2026 Best Aircraft Taper Routers for Global Buyers

Material-density guide for selecting, using, and maintaining an aircraft taper router

How to use this chart: Higher-density materials generally require more rigid tool control, sharper cutters, appropriate feed rates, and better heat management. Aluminum alloys are widely used for airframes and are comparatively easy to machine, while titanium requires lower cutting loads, effective cooling, and slower material removal.

Selection and maintenance: Choose a taper router with suitable collet accuracy, variable-speed control, adequate power, and compatible carbide tooling. Before each operation, inspect the cutter, collet, air passages, bearings, and guards. Clean chips after use and follow the tool manufacturer’s lubrication and service schedule.

Material densities are nominal engineering values: aluminum 2024-T3, aluminum 7075-T6, titanium Ti-6Al-4V, stainless steel 316, and carbon-fiber/epoxy laminate. Composite density varies with fiber content and layup.

FAQS

Which specifications matter when comparing an aircraft taper router?

Check spindle speed, motor power, collet range, taper-angle control, feed rate, and positional repeatability. A practical spindle range is near 10,000–30,000 rpm. Repeatability below 0.05 mm supports controlled composite trimming. Higher speed is not always better.

Is faster spindle speed always the best choice?

No. Excessive speed can create heat and soften resin. That may damage a clean edge. Measure surface temperature during a witnessed cutting trial. Speed alone can mislead.

What motor power suits common composite panels?

A 2.2–3.0 kW motor may handle common composite panels. Thick laminates need testing with the actual cutter and material. Check edge quality, cycle time, and tool wear. Do not trust a brochure alone.

Which safety features should buyers inspect?

Look for an enclosed cutting area and reliable emergency stop. Stable workholding prevents unexpected movement. Guarded access points protect operators during cutting. Effective dust extraction keeps the workspace cleaner. Noise data should be measured, not merely described as quiet.

What documents should accompany the machine?

Request electrical conformity documents, risk assessments, factory test records, and calibration reports. Confirm that certificates cover the complete machine. Individual component documents may not be enough. Check serial-number traceability and maintenance records. Technical translations can still be unclear.

How can buyers evaluate workshop reliability?

Inspect calibration records, emergency-stop design, dust containment, and local electrical compatibility. Sealed linear guides help in dusty environments. Ask about remote diagnostics and service access. A heavy cutting head may create small errors after repeated passes. Ergonomics deserves more attention than I once assumed.

Can a five-axis router improve production?

A five-axis option can reduce repositioning and improve access to complex surfaces. It also adds setup complexity and training requirements. Compare the time saved against operator skill demands. More axes are not automatically better.

How should total ownership cost be calculated?

Include freight, import duties, commissioning, tooling, training, energy, calibration, and expected downtime. Also calculate spare-part and service costs. Ask how quickly a replacement spindle or control board can arrive. The cheapest quote may become expensive after one missed production week. I would still request references from similar climates. That step takes time.

Conclusion

Aircraft Taper Routers are specialized cutting tools designed to create smooth, controlled tapers, countersinks, and precision openings in aircraft structures and related components. Their main applications include preparing holes, fitting fasteners, shaping composite panels, and working with materials such as aluminum alloys, titanium, plastics, and fiber-reinforced composites. Different router types vary in cutting geometry, drive method, speed control, and compatibility with specific materials, so selecting the correct tool is essential for accuracy and surface quality.

When comparing the best 2026 models, global buyers should evaluate speed range, power, runout, ergonomics, depth control, dust management, durability, and available accessories. Safety features, conformity with applicable standards, reliable supply, warranty support, replacement parts, shipping, and total ownership cost are equally important. Proper selection should be followed by correct setup, suitable cutting parameters, protective equipment, routine cleaning, cutter inspection, lubrication where appropriate, and scheduled maintenance to preserve performance and extend service life.
Clara

Clara

Clara is a seasoned marketing professional with a strong understanding of customer needs, market trends, and the practical value of innovative business solutions. As a key contributor to the company’s content and communication strategy, she regularly updates the company website with insightful blog......